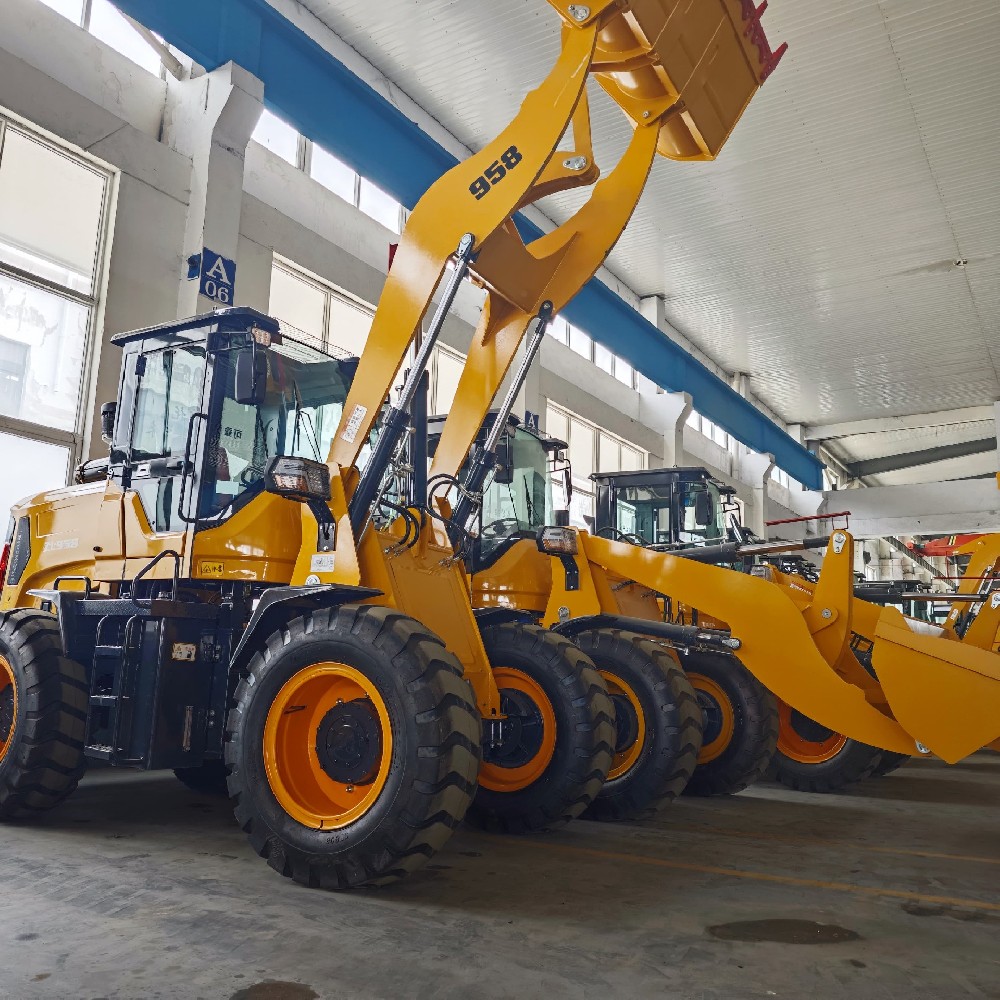
Export supply is rarely a single shipment. A dealer in one country, a contractor in another and a rental fleet somewhere else all want different things from the same machine, and the supplier has to hold those differences together without losing consistency in the product itself.
Mingyi Machinery treats overseas cooperation as a long working relationship rather than a one-off order. The conversation starts before the specification is fixed, and it continues well after the machine has been unloaded.
This page sets out how that cooperation is organised: how configuration is matched to a market, how OEM and ODM work is handled, what documentation and training come with the machine, and how after-sales and parts supply are kept moving.
What long-term cooperation looks like in practice
Export supply works best when both sides treat the first order as the beginning of a working relationship rather than the whole of it. A dealer who intends to sell a model again next year needs the second machine to match the first one, down to the hose routing and the position of the service points.
That expectation shapes how we plan. Configuration decisions are recorded against the dealer and the model, so a repeat order can be built the same way without the customer having to re-explain a requirement that was already settled months earlier.
Long-term cooperation also means saying what a machine will not do. Overpromising on a first enquiry tends to produce a difficult second conversation, and a partner who trusts the answer is worth more than an extra order taken under the wrong assumption.
The practical result is a shorter path from enquiry to shipped unit on every subsequent order, because the specification, the documentation set and the parts list are already agreed.
Matching machine configuration to a local market
The same base machine can be right for one market and wrong for another. Local fuel quality, operator habit, prevailing ground conditions and the jobs the machine is actually bought for all pull the specification in different directions.
Engine preference is often the first point of discussion, since service networks and familiarity vary by region. Cab specification, air conditioning, lighting and the guarding expected on site follow close behind.
Attachment habits differ just as much. In some markets a compact carrier is bought almost always with a breaker, in others with an auger or a grab, and the hydraulic provision needs to suit the attachment that will actually be used.
Documentation language and the format of the parts book matter more than they appear to. A dealer whose technicians cannot read the manual will end up calling for help that a clearer document would have prevented.
OEM and ODM work: from requirement to shipped unit
OEM and ODM enquiries start from different places. An OEM partner usually has an established product and wants it built to their drawing and their brand, while an ODM buyer has a market gap and expects the factory to propose a machine that fills it.
Either way the work begins with the requirement written down: duty cycle, ground conditions, the jobs the machine must cover, the standards it has to meet and the brand elements that must appear on the finished unit.
Drawings, samples or photographs are then exchanged until both sides are describing the same machine. Approvals are recorded in writing, because a change agreed verbally tends to resurface as a dispute once the unit is on the water.
Brand elements, colour, decals and the nameplate are agreed before production starts. Changing them afterwards is possible but slow, and it usually means reworking parts that have already been painted.
Documentation, parts books and technical information
A machine arrives with more than steel and hydraulics. The parts book, the maintenance schedule, the hydraulic schematic and the wiring diagram are what let a dealer keep it working after the sale.
We treat those documents as part of the delivery, not as an afterthought. Part numbers on the book match the numbers used when a dealer orders spares, which is the single detail that most often decides whether a parts order goes smoothly.
Maintenance intervals are stated in operating hours and in plain language, so a workshop that has never seen the model can still carry out the first service correctly.
Where a market needs the manual in its own language, that is arranged as part of the order rather than left to the dealer to solve after delivery.
Training for dealer technicians and end users
A dealer workshop that understands the machine sells it with more confidence and handles the first service visit without waiting for support. Training is therefore aimed at technicians first and operators second.
Sessions cover the service points, the checks that belong to each interval, the adjustment procedures and the fault-finding path for the complaints that come up most often. The aim is independence, not dependence on a call back to the factory.
Remote sessions work well for follow-up questions, particularly when a technician can show the machine on a phone camera while the fault is happening.
Operator guidance focuses on the habits that protect the machine: warm-up, correct attachment fitting, and the daily checks that catch a small problem before it becomes a failed component.
After-sales coordination and spare parts flow
After-sales support is mostly a logistics problem. The question a dealer asks is not whether a part exists, but whether it can be identified, packed and sent before the machine loses too many working days.
For that reason we recommend a stocking list at the time of the first order, built around wear parts and the items most likely to be needed in the first season of work.
Warranty claims follow a written route with photographs and a description of the failure, so that the decision does not depend on who happens to be available on the day.
A single contact point keeps this moving. When several people are involved on both sides, the same question gets answered twice and the machine waits while the answers are reconciled.
Communication routines that keep a project moving
Distance and time zones are the two things that slow export work down more than any technical problem. A routine handles them better than goodwill does.
We work with one named contact on each side, written confirmation of every specification change, and photographs or short video from the workshop when a question is easier to show than to describe.
Questions are answered in one consolidated message rather than in fragments, which makes it possible to act on the answer without hunting through a long thread.
Where a decision has a deadline, the deadline is stated up front. Most delays in this work come from a choice that nobody knew was blocking the order.
Field feedback reaching the workshop
The most useful design information arrives from machines that are already working. A dealer reporting the same complaint on several units is describing something the workshop needs to change, not a series of isolated faults.
We collect that feedback through the service route and through the parts orders, since an unusual number of the same component is itself a signal.
Where a change is justified, it goes into production with a record of what was altered and from which batch, so a later parts order can be matched to the machine that is being repaired.
The loop closes when the dealer is told what changed and why. That is what turns a complaint into a reason to keep buying the model.
What to look for in a manufacturing partner
Consistency is the first thing worth checking. A factory that builds the same model the same way every time is easier to support than one that produces a better machine on a good day.
Willingness to document is the second. A supplier who can produce the schematic, the torque figures and the parts numbers on request will save a dealer more time than any feature on the specification sheet.
Reach after the sale is the third, and it is the one most often discovered too late. The right question is not whether the supplier answers quickly during the sale, but whether the answer still comes quickly once the machine is working.
Partners who think in years rather than orders tend to ask better questions at the start. That is usually the clearest sign of how the relationship will go.
Consistency across repeat orders
A dealer ordering the same model a second time expects the second machine to match the first. That expectation covers the visible parts and the ones underneath: hose routing, the position of the service points and the behaviour of the controls.
Configuration is therefore recorded as a reference rather than rebuilt from memory, so a repeat order is produced against the same description the first one was.
Where a running change has been made, the dealer is told before the order is confirmed. A machine arriving slightly different from the previous one is fine when it is expected and a problem when it is not.
Consistency also makes the parts stock simpler. When several machines in a market share one configuration, a single stocking list covers the whole fleet.
Changing a specification after production starts
Changes are easiest before the machine reaches the line and hardest once it has been painted. That is the reason to push the specification conversation early rather than to resist changes in principle.
When a change is requested mid-build, the first step is to establish what it affects: parts already fitted, parts already bought in, and the documents that have to be reissued.
The options are then set out plainly, including the effect on the shipping date. Most customers decide quickly once they can see how much time the change will take.
Every agreed change is confirmed in writing and added to the order record, so the machine that arrives is the machine that was discussed.
Working with rental fleets
Rental buyers ask different questions from contractors. They care about how quickly a machine can be prepared for the next hirer, how forgiving it is of a varied operator, and how fast a damaged part can be replaced.
Fleet machines benefit from simple, robust preparation: guards that survive being loaded, service points that are easy to find, and a parts list that covers the items most often damaged on hire.
Documentation for a fleet is aimed at the yard staff who prepare the machine between hires, not only at the technician who services it.
Where several units go into the same fleet, they are built to one configuration so that training, spares and preparation are identical across the set.
How a new dealer starts
A new relationship usually begins with one or two machines rather than a container. That first order is as much a test of the working relationship as of the product.
We use it to settle the practical things: who the contacts are, how specification changes are confirmed, what documents come with the machine and how a parts order is raised.
The first machines are also the moment to agree the stocking list and to arrange any technician training, while the units are still being built.
If those mechanics work, the second order is straightforward. If they do not, it is better to find out on two machines than on twenty.
Visiting the factory and seeing the line
A visit settles more questions than a correspondence. Walking the assembly line shows how machines are built, what is checked and how a custom configuration is handled.
Visitors usually want to see the inspection area and the test bay, which is the right instinct. Those two places tell more about a supplier than any presentation.
Visits also let both sides settle the configuration face to face, with the machine in front of them rather than a drawing on a screen.
Where a visit is not practical, a live video walk-through of the relevant areas works nearly as well, and we arrange it often.
Protecting a partner's own design
An OEM partner bringing their own drawings and their own brand is trusting the factory with information that matters to their business.
That information is treated as theirs: drawings, specifications and photographs are held for the purpose of building their machines and not used elsewhere.
Agreements covering this are straightforward and worth having in writing before work starts, particularly where a design is distinctive.
In practice the arrangement is simple. A partner who is comfortable sharing detail gets a better machine, because the detail is what makes it theirs.
Related pages
Mini Excavators · Skid-Steer Loader · 4x4 Rough Terrain Forklift · Loaders · three tonne small excavator · mini excavator manufacturer for export · mini skid steer loader · compact skid steer loader · About Mingyi Machinery · Contact Mingyi Machinery